| 1 | Introduction and quick start What the tool is, what it covers, the screen, one spool in five steps | |
| 2 | Inputs, field by field Every field and component card: meaning, unit, default, limits | |
| 3 | How the estimate is calculated Cut lengths, welds, weights, man-hours, cost, schedule, with figures | |
| 4 | Outputs Tabs, drawings, PDF report, Excel, Word, MTO, ids and verification | |
| 5 | Worked example SP-101 cooling-water spool, every number shown | |
| 6 | Limits and questions What is not covered, messages, frequent questions, glossary |
The Estineer Pipe Spool Fabrication tool prices the shop fabrication of one pipe spool and produces its fabrication drawings. You copy the spool from the client's isometric: the material, size, schedule and flange class, then each component in fabrication order, from the start face to the finish face. The tool builds the spool in 3D, cuts the pipe into pieces, lists every weld, takes the weights and prices from its catalogue, builds the man-hours activity by activity and turns them into a cost, a price and a schedule.
The design is by others. The tool does not size the pipe or check it for pressure, stress or support: the line class and the isometric come from the client's piping design. It does check what matters to the workshop: pieces too short to weld, the transport envelope, the shop test pressure against the flange class, heat treatment and the NDT scope.
The same model drives the 3D view, the drawings, the report and the Excel and Word files. Change a field and all of them change together. Enter the same inputs twice and you get the same result; every purchased report carries a check code that proves which inputs, engine version and database produced it.
| Item | Covered |
|---|---|
| Spool | One shop-fabricated spool: straight runs, elbows, reducers, tees, half couplings, olets, end flanges |
| Size | NPS ½ to 24 for the run; branches and olets down to NPS ½ |
| Construction | Butt-welded ASME B16.9 fittings above NPS 1½; socket-weld ASME B16.11 Class 3000 at NPS 1½ and smaller |
| Materials | Carbon steel (A106 B seamless or A53 B ERW), low-temperature carbon steel (A333 Gr 6), stainless 304L and 316L |
| Flanges | ASME B16.5 weld neck, slip-on, socket weld and blind, Class 150 to 1500 |
| Route | Up to 12 straight runs of 20 mm to 12 m each, and up to 6 branches |
| Finish and test | Blast and paint systems for carbon steel, pickling and passivation for stainless, NDT by method, shop hydrotest, preheat and PWHT |
| Subcontract | Painting, hydrotest and NDT can be priced from a subcontractor's quote instead of in-house work |
| Currency | AUD by default, any currency by exchange rate; prices exclude GST and tax |


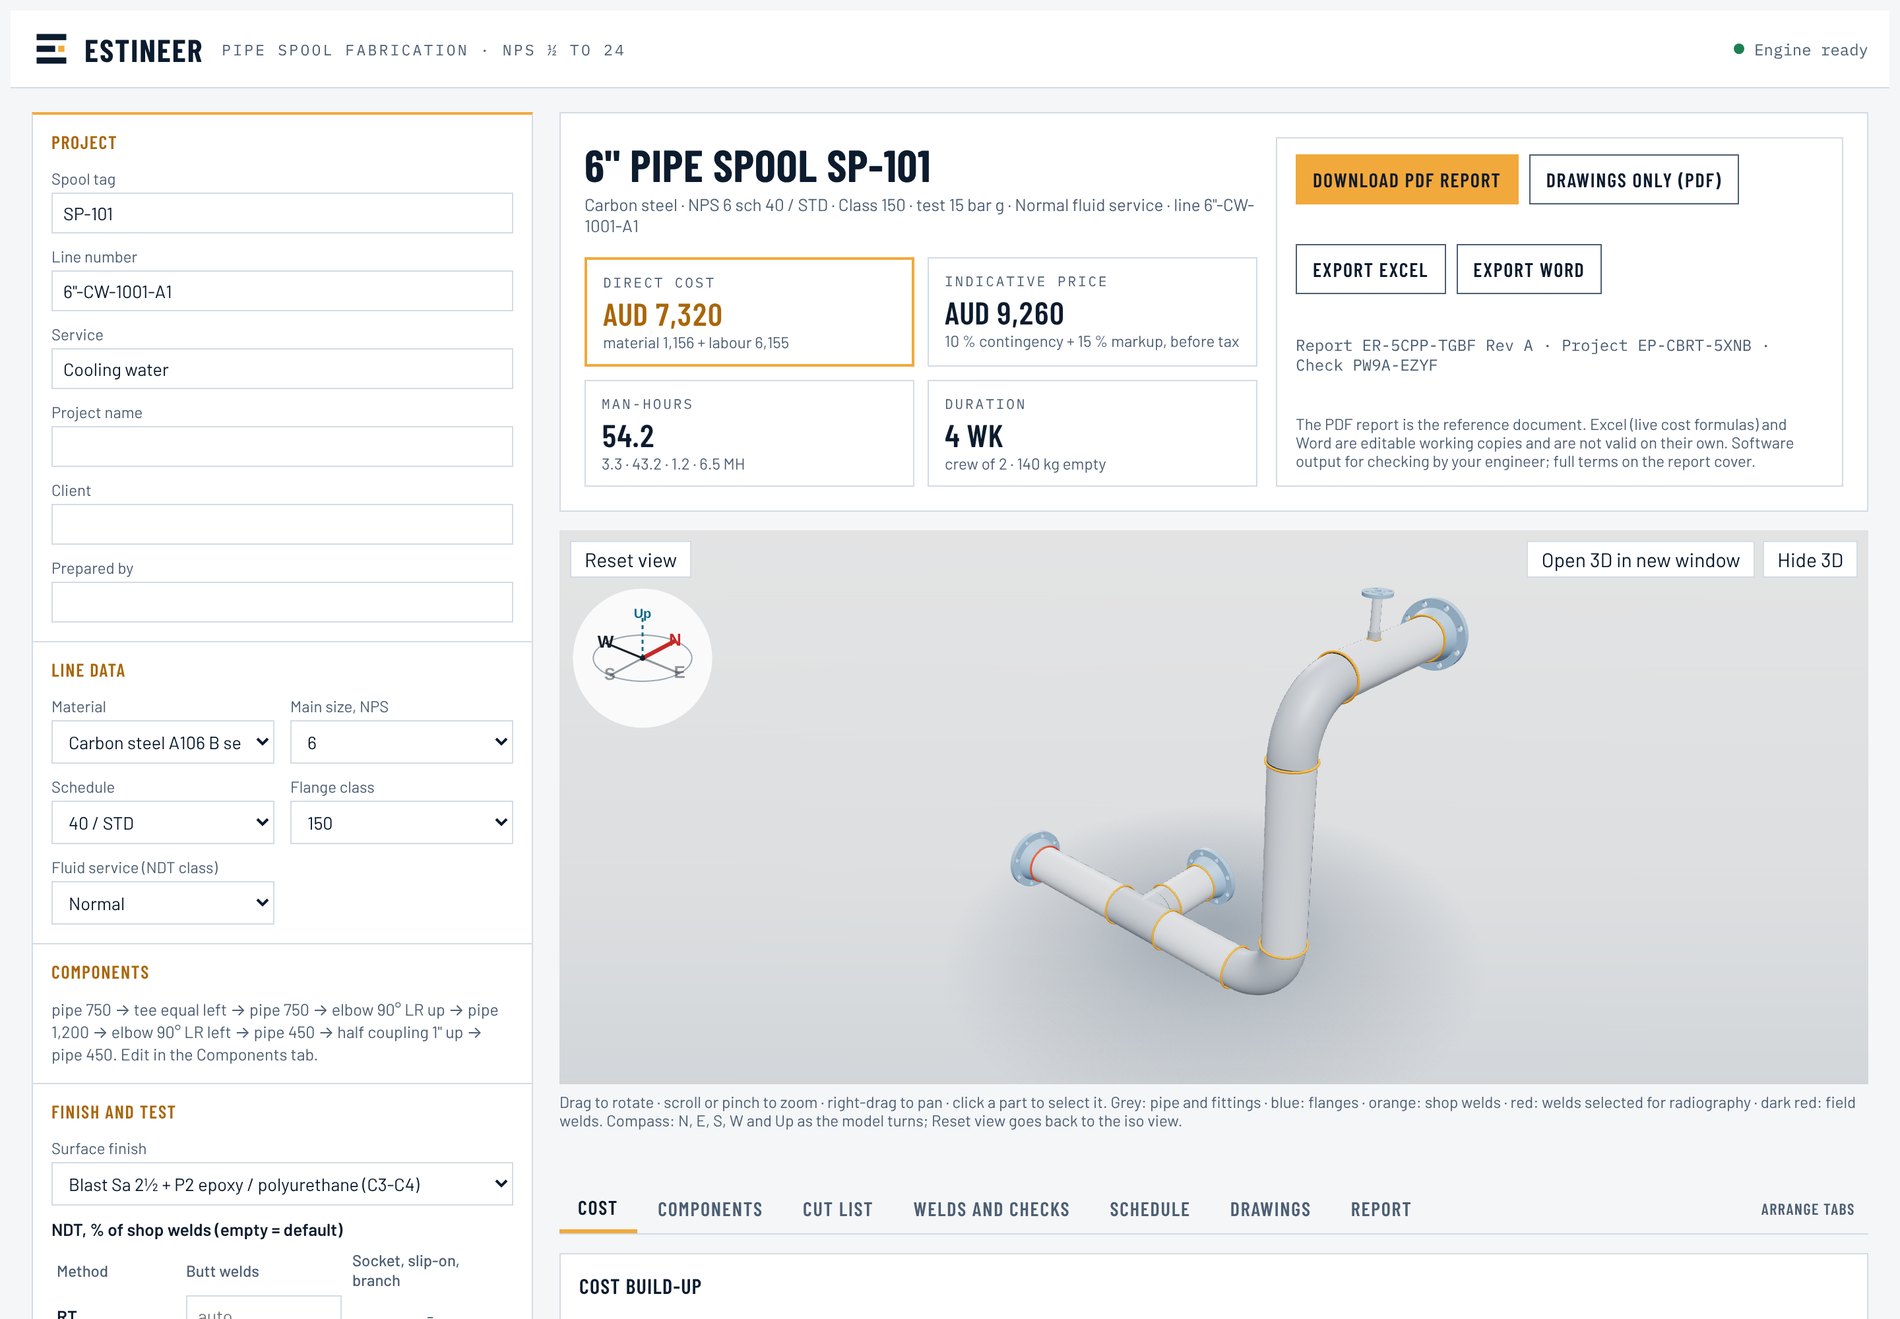
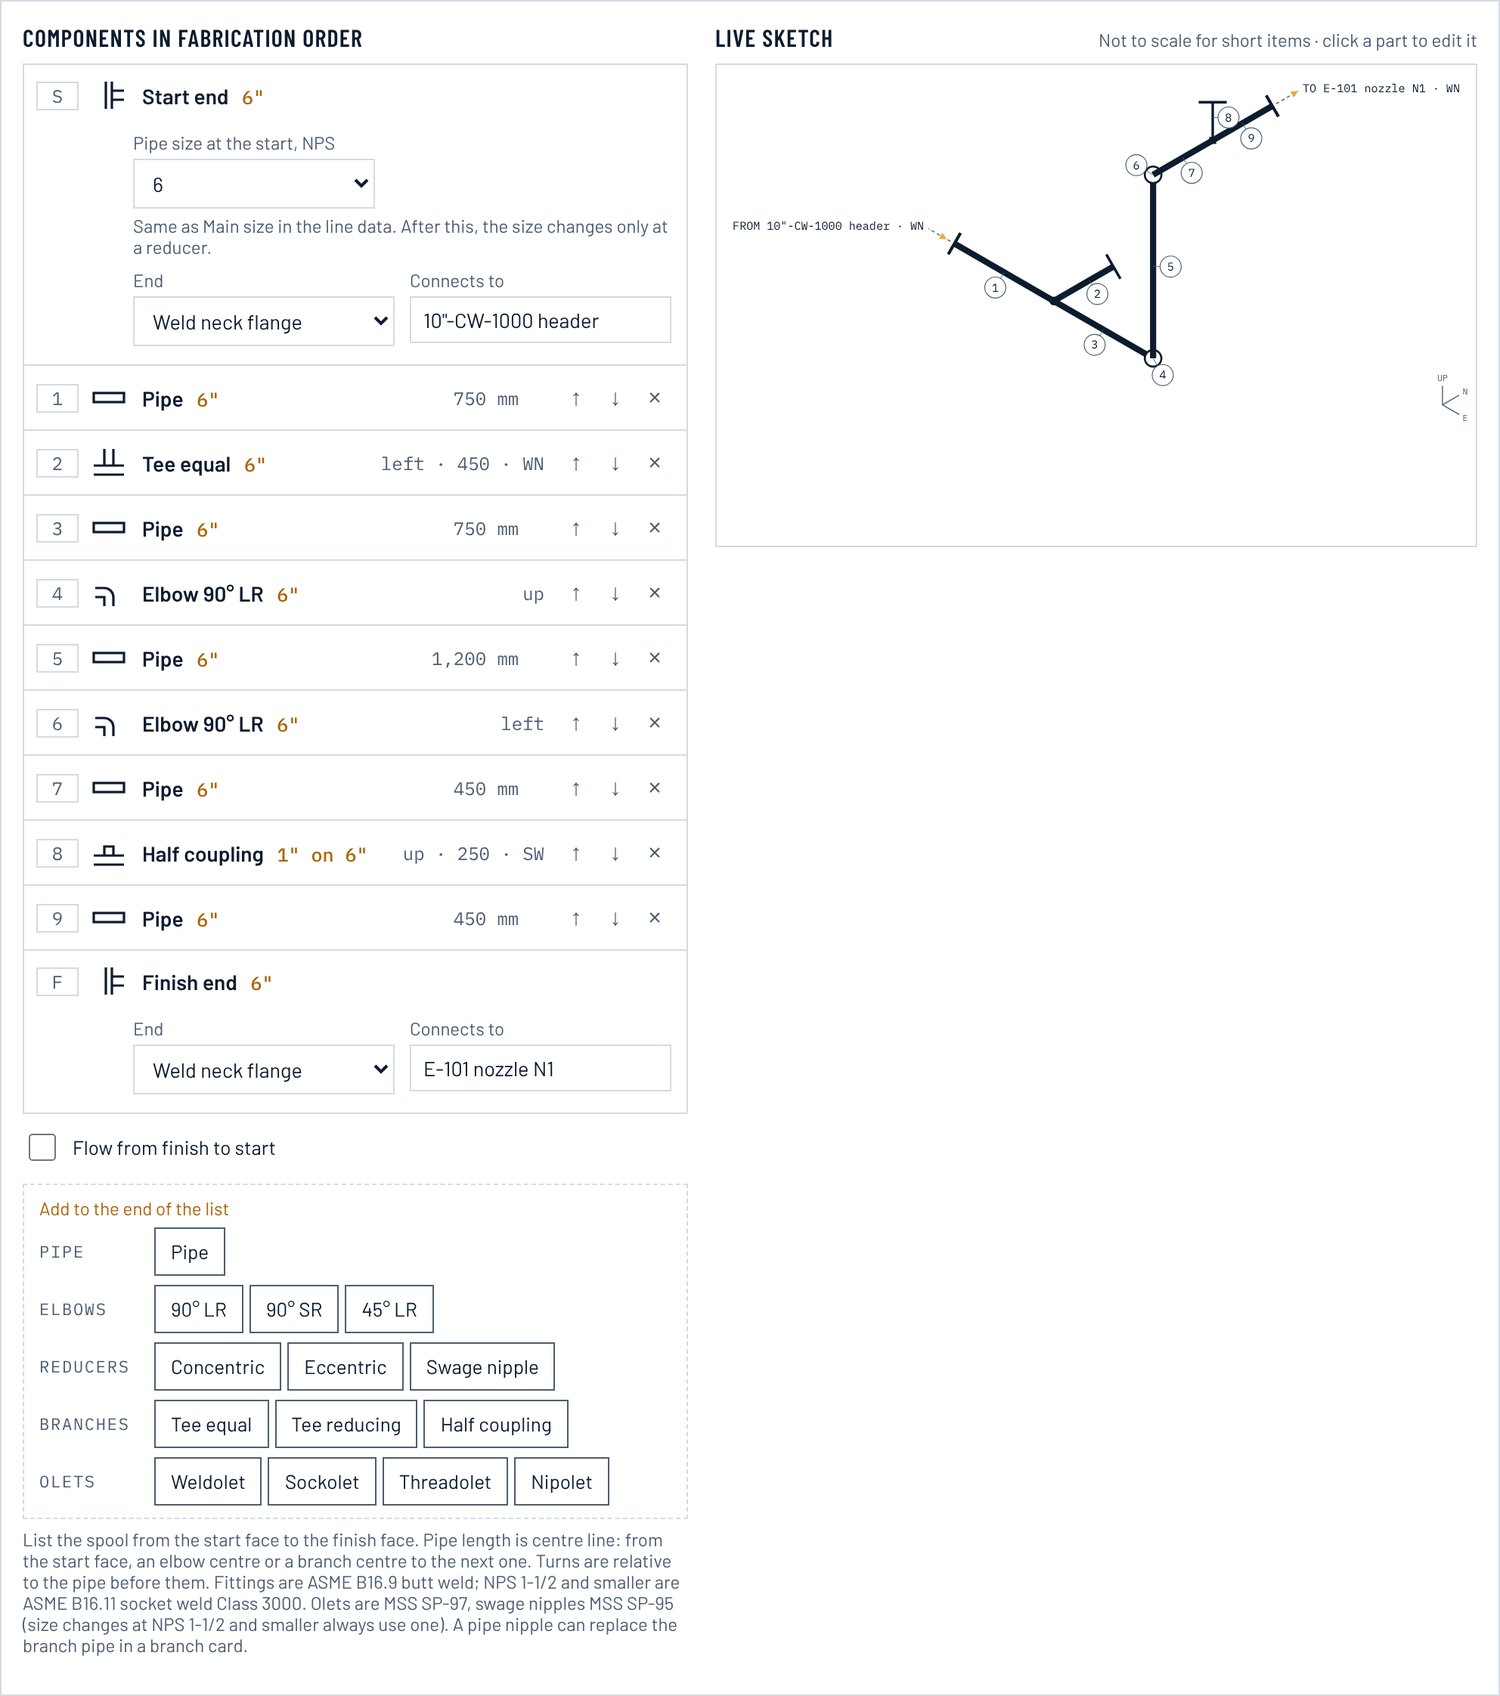
12345678910Figure 1.3 The tool page with the SP-101 example loaded. The numbers match the key below.
| Step | What to do |
|---|---|
| 1 | Project. Enter the spool tag and the line number exactly as on the isometric. Project name, client and prepared by go on the report cover; leave them empty and the cover leaves them blank. |
| 2 | Line data. Choose the material, the main size (the size at the start face), the schedule and the flange class from the line class. Choose the fluid service: it sets the default radiography. |
| 3 | Components. Open the Components tab. Set the start end and what it connects to. Then add the cards in fabrication order with the buttons at the bottom: pipe, elbow, reducer, branch or olet. Pipe lengths are centre-line lengths from the isometric. Finish with the end type at the finish face. The sketch beside the cards updates as you type; click a part of the sketch to edit its card. |
| 4 | Finish and test. Choose the surface finish, the hydrotest pressure from the client's line list, and any NDT the client asks for. Leave NDT empty to use the default for the fluid service. |
| 5 | Rates and price. Check the workshop rates, contingency and markup. Read the result cards, the Cost tab and the alerts; then download the report and drawings. |
On estineer.com the tool is free to use on screen. The cost, man-hours, weights, bill of materials, cut list and weld register are shown in full.
| Free preview on screen | Purchased report | |
|---|---|---|
| Cost, price, man-hours, BOM, cut list, welds | Full | Full |
| Drawings | First sheet, low resolution, marked PREVIEW | Four clean A4 vector sheets |
| Report | Cover page only | Complete PDF |
| Excel, Word, MTO | Not available | Live-formula workbook, editable Word file, MTO in Excel and CSV |
| Ids and verification | None | Report id, project id and check code |
To buy, press a download button, sign in with a code sent to your email and pay by card. Files are produced on the server after payment, you receive a tax invoice and you can download again for 12 months. Prices and offers are shown on the site at the time of purchase.
The form on the left holds the spool-wide data. The components themselves are cards in the Components tab. Every field is named here exactly as on screen. Where a field has a default, leaving it empty uses the default.
| Field | Meaning | Default / limit |
|---|---|---|
| Spool tag | The spool number from the isometric. Printed on every drawing and file name. | Up to 24 characters |
| Line number | The line the spool belongs to, for example 6"-CW-1001-A1. | Free text |
| Service | What flows in the line. Shown in the title and on the report. | Free text |
| Project name, Client, Prepared by | Printed on the report cover table and the Word cover. Empty fields print blank. | Optional |
| Field | Meaning | Options |
|---|---|---|
| Material | Sets the pipe, fitting and flange specifications, the filler metal, the material factor on welding hours and the finishes on offer. | Carbon steel A106 B seamless; carbon steel A53 B ERW; low-temperature CS A333 Gr 6; stainless 304L; stainless 316L |
| Main size, NPS | The pipe size at the start face. The size changes along the spool only at a reducer or swage nipple card. | NPS ½ to 24 |
| Schedule | Wall schedule from the catalogue for the material and size. Fittings follow the pipe wall. | As listed for the size |
| Flange class | ASME B16.5 pressure class of every flange on the spool. | 150, 300, 600, 900, 1500 |
| Fluid service (NDT class) | Sets the default radiography of butt welds. | Normal 5 %; Category D 0 %; Category M 20 %; Severe cyclic 100 % |
| Material | Pipe | Fittings | Flanges | Filler |
|---|---|---|---|---|
| CS seamless | A106 Gr B | A234 WPB | A105 | E7018 / ER70S-6 |
| CS ERW | A53 Gr B ERW | A234 WPB | A105 | E7018 / ER70S-6 |
| LTCS | A333 Gr 6 | A420 WPL6 | A350 LF2 Cl 1 | E7018-1 / ER70S-6 |
| SS 304L | A312 TP304/304L | A403 WP304/304L | A182 F304/304L | ER308L |
| SS 316L | A312 TP316/316L | A403 WP316/316L | A182 F316/316L | ER316L |
The Components tab lists the spool in fabrication order, from the start face to the finish face. Each card is one item. Use the arrows to move a card, the cross to delete it, and the buttons at the bottom to add a card at the end of the list. Click a card, or a part of the live sketch, to open it for editing.

| Card | Fields | Notes |
|---|---|---|
| Start end / Finish end | Pipe size at the start; end type; Connects to (text on the drawings) | End types below |
| Pipe | Length, mm (centre line) | 20 mm to 12,000 mm per straight run |
| Elbow | Type: 90° LR (1.5 D), 90° SR (1.0 D), 45° LR; Turn | ASME B16.9 / B16.11 |
| Reducer | Type: concentric, eccentric (flat on top or bottom), swage nipple; Outlet size, NPS | Swage nipples are MSS SP-95; used automatically where the big end is NPS 1½ or smaller |
| Tee equal / Tee reducing | Branch size; Branch direction; Branch pipe (pipe or nipple 75, 100, 150 mm); Branch length, mm; Branch end; Connects to; Flows in or out | Branch length is from the run centre line to the branch end face |
| Half coupling | As a branch; branch end usually socket weld | Class 3000, welded to the run with a hole cut |
| Weldolet, Sockolet | As a branch | MSS SP-97; the olet sits on the run pipe |
| Threadolet, Nipolet | Branch size and direction | The NPT thread or the 89 mm plain end is the branch end; the connection is by others |
| End | What the tool adds |
|---|---|
| Weld neck flange (WN) | B16.5 weld neck flange, one butt weld, hydrotest end with a test blind |
| Slip-on flange (SO) | B16.5 slip-on flange, two fillet welds; pipe set back by the wall thickness + 3 mm |
| Socket-weld flange (SW) | B16.5 socket-weld flange (NPS 3 and smaller), one socket weld with a 1.6 mm gap |
| Weld neck + blind (BL) | Weld neck flange plus a blind flange, gasket and bolts fitted in the shop |
| Bevelled end (BE) | No item; the end is bevelled for a field weld; hydrotest with a test plug |
| Plain end (PE) | No item; plain end for a field socket weld |
| Cap | B16.9 butt-weld cap (or B16.11 socket-weld cap at small sizes) |
| Field | Meaning | Default / options |
|---|---|---|
| Surface finish | Carbon steel: abrasive blast to Sa 2½ plus a paint system. Stainless: pickling and passivation inside and outside. | CS: P1 alkyd, P2 epoxy/polyurethane, P3 zinc silicate/epoxy/polyurethane, P5 silicone aluminium, P6 phenolic epoxy (CUI), none. SS: pickle, none |
| NDT, % of shop welds | Six fields: RT and UT for butt welds; MT and PT for butt welds and for socket, slip-on and branch welds. Empty uses the default. | RT default by fluid service; MT on carbon steels only (MT on stainless is refused) |
| Per-weld NDT | In the Welds tab you can tick the methods weld by weld; those welds are marked as set by you. | Optional |
| Shop hydrotest | Includes the shop hydrotest with test blinds or plugs at every end. | On |
| Test pressure, bar g (client) | From the client's line list. Checked against 1.5 × the flange rating at 38 °C. | Above 0, at most 400; empty uses 15 bar g with an alert |
| PWHT | Post-weld heat treatment. Auto suggests it for carbon steel walls above 19 mm. | Auto, yes, no |
| Preheat, °C | Empty uses the suggested value (79 °C on carbon steel walls above 25 mm). | 5 to 300 °C |
| Insulated in service | Information only (insulation is by others); suggests a coating for use under insulation. | Off |
The tool chooses which welds get NDT: the largest and thickest first, until the percentage is reached. Radiography uses the butt welds of the run; MT and PT on “other” welds cover socket, slip-on and branch welds.
Painting (or pickling), hydrotest and NDT can each be bought from a subcontractor. Tick the scope and enter the quote in the report currency. The tool then removes the in-house hours and materials of that scope and adds the quote as a cost line “(subcontract)”. Tick it with no amount and the scope is listed under “The price excludes”. Amounts must be zero or more.
| Field | Meaning | Default | Allowed |
|---|---|---|---|
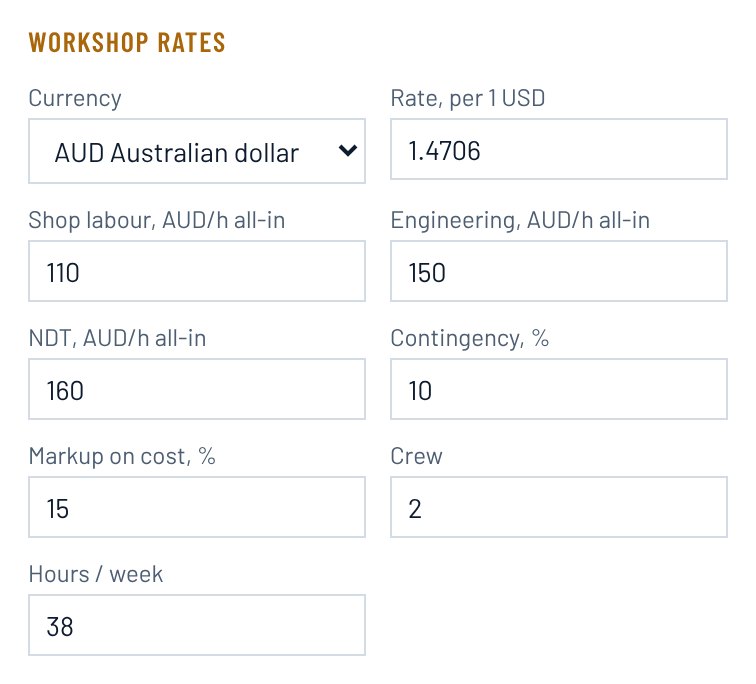
| Currency, Rate per 1 USD | Report currency and its exchange rate. Catalogue prices are in USD. | AUD, 1.4706 | Rate above 0 |
| Shop labour, /h all-in | Fitters, welders, helpers, painters, test crew. | 110 | Above 0 |
| Engineering, /h all-in | Spool drawing check, weld map, test pack, data book. | 150 | Above 0 |
| NDT, /h all-in | In-house NDT technicians. | 160 | Above 0 |
| Contingency, % | On the direct cost. | 10 | 0 to 100 |
| Markup on cost, % | On cost plus contingency. | 15 | 0 to 100 |
| Crew | People working on the spool at the same time; sets the duration only. | 2 | 1 to 50 |
| Hours / week | Working hours per week; sets the duration only. | 38 | 1 to 84 |

This chapter explains each step from the cards to the price. The tool does not design the pipe: there are no wall-thickness or stress calculations. The calculations are those of a fabrication estimate, and every allowance the tool assumes is printed in the report under “Basis of estimate”.
The cards are walked from the start face. Each pipe card moves along the current direction by its centre-line length; each elbow turns the direction; each branch card places a branch at the current point. Fitting dimensions come from the catalogue tables: ASME B16.9 elbows, tees, reducers and caps; ASME B16.11 socket-weld fittings; ASME B16.5 flanges; MSS SP-97 olets and SP-95 swage nipples. The result is a 3D route with every item and every joint located.
Take-outs: elbow centre to end; tee centre to end (run) or centre to branch end; reducer length; flange length Y for weld neck; socket depth less a 1.6 mm gap for socket welds; for slip-on flanges the pipe stops short of the face by the wall thickness + 3 mm. The root gap is 2 mm, so each bevelled end loses 1 mm. A piece shorter than 50 mm gives a warning (hard to weld); a straight run that cannot hold its fittings stops the run.
Example (SP-101, first piece): L = 750 mm from the start face to the tee centre; weld-neck flange Y = 89 mm; 6" tee C = 143 mm; two bevelled ends 2 × 1 mm. Cut length = 750 − 89 − 143 − 2 = 516 mm, as in the Cut list tab.
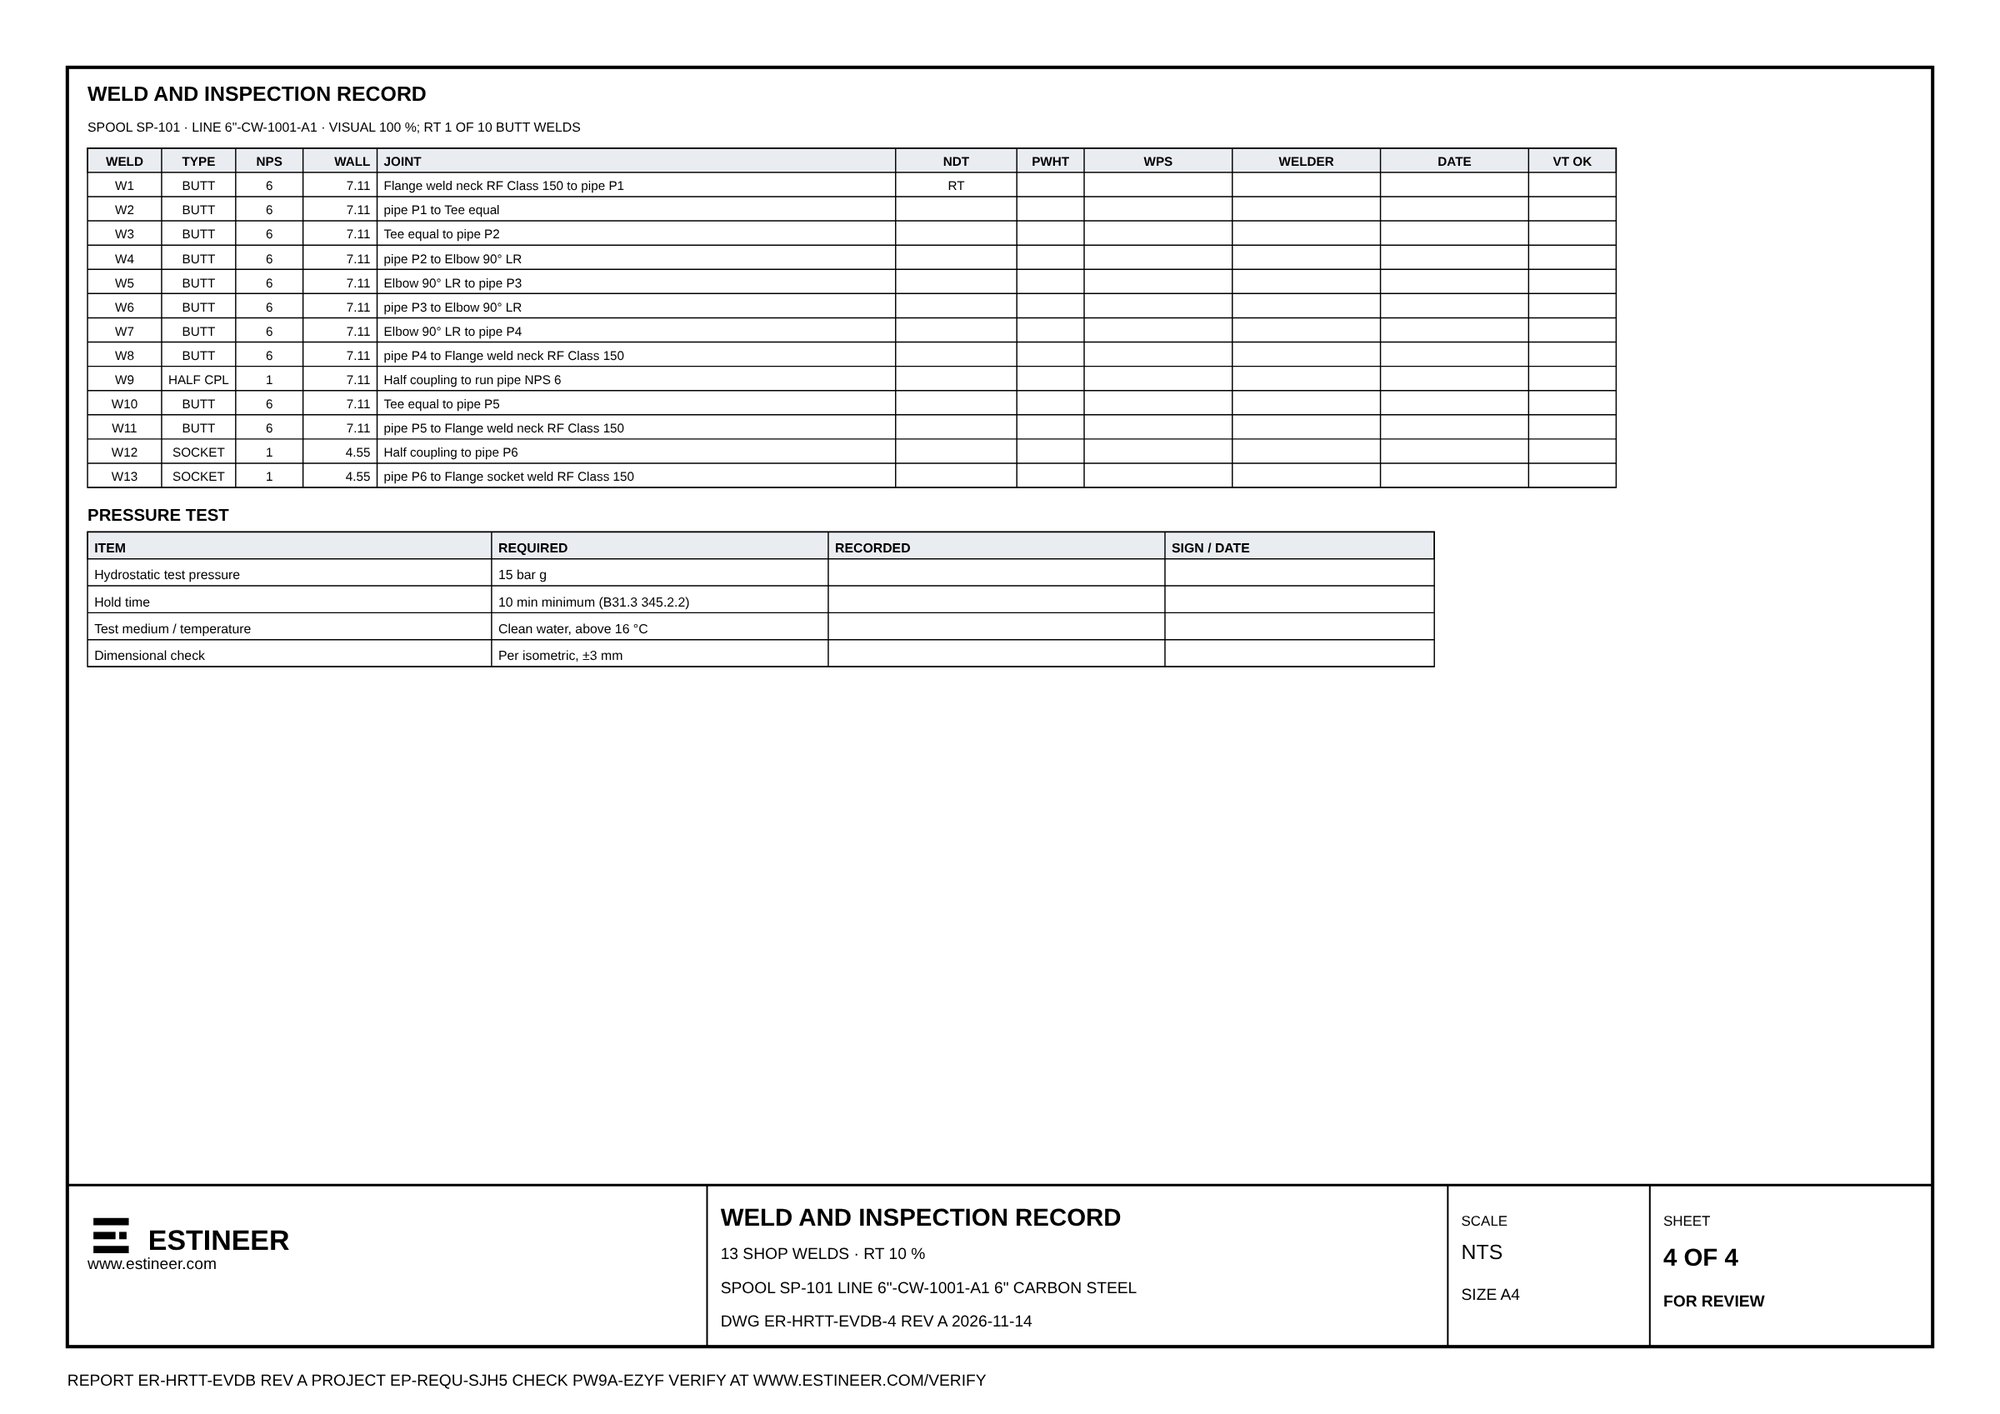
Every joint between two items is a weld: pipe to fitting, fitting to fitting, flange to pipe. Branch welds join a half coupling or an olet to the run pipe, with the hole cut included. Field welds at bevelled ends are listed but not priced. The register numbers the shop welds W1, W2 … in fabrication order; the same numbers appear on the 3D view, the isometric and the weld and test record.
The material take-off groups the items by size and description: pipe in metres (with the cutting loss), fittings and flanges in each, welding consumables in kg (from the weld size and count), abrasive and paint by area. Prices are catalogue prices in USD multiplied by the exchange rate. A catalogue item with no price is listed under “The price excludes”, never silently priced at zero.
The man-hours are built activity by activity. Each activity has a quantity, a unit rate from the Estineer man-hour tables and a material factor:
| Activity | Quantity and unit | Stage |
|---|---|---|
| Handling | metres of pipe by size and schedule | Shop |
| Cutting, bevelling | one cut per piece; one bevel per butt-welded end | Shop |
| Butt welds | per joint, by size and wall | Shop |
| Flange attachment | weld neck (with its butt weld), slip-on (two fillets), socket weld | Shop |
| Branch welds | half coupling or olet, including the hole | Shop |
| Socket welds | per joint, Class 3000 | Shop |
| Preheat, PWHT | per weld, when used | Shop |
| Blind bolting | 0.1 MH per bolt | Shop |
| Blasting, painting | outside area; 0.08 MH per m² per coat | Shop |
| Pickling (stainless) | inside and outside area, 0.15 MH per m² | Shop |
| QC | 0.5 MH + 0.05 MH per joint: fit-up, marking, dimensional check | Test |
| Hydrotest | per end: flanged end or plugged end, by size | Test |
| NDT | per weld examined, by method and size | NDT |
| Engineering | 2 MH + 0.1 MH per weld: drawing check, weld map, test pack, data book | Engineering |
| Material | Handling, cutting | Welding | Extra per joint |
|---|---|---|---|
| Carbon steels | 1.00 | 1.00 | 0 |
| Stainless 304L, 316L | 1.20 | 1.46 | 0.6 h |
The NDT percentages apply to the count of welds in each group. The tool picks the welds, largest and thickest first, and lists them in the weld register; welds you tick yourself are kept. The hydrotest is priced per end (flanged ends with a test blind, plain or bevelled ends with a test plug). Category M adds a sensitive leak test at half the hydrotest hours. A subcontracted scope replaces these hours by the quote.
The price excludes GST and tax, transport, site work and anything listed in the red box “The price excludes”.
For SP-101: Drawing approval from week 0.0 for 0.5; Material procurement from week 0.5 for 2.0; Fabrication, NDT and test from week 2.5 for 1.0; Finishing and dispatch from week 3.5 for 0.5. Duration 4 weeks. Crew and hours per week change only the duration, never the cost.
| Check | Rule |
|---|---|
| Pieces between welds | Each straight run must hold its fittings; a piece under 50 mm gives a warning |
| Transport | The spool envelope against 12.0 × 2.4 × 2.6 m, a standard truck without a permit |
| Shop test pressure | At most 1.5 × the flange rating at 38 °C for the class |
| Heat treatment | PWHT suggested for carbon steel above 19 mm; preheat suggested above 25 mm; confirm with the WPS |
| Materials | MT is refused on stainless; LTCS needs impact-tested procedures (noted) |
Points the client or the welding engineer must confirm are listed as open items, in amber; they do not stop the estimate.
Four cards sit under the title: Direct cost (materials + labour), Indicative price (with the contingency and markup used), Man-hours (engineering, shop, NDT and test) and Duration (weeks, with the crew and the empty weight). Alerts appear above the 3D view: yellow points to confirm, red where a check fails or the input was refused.
| Tab | What it shows |
|---|---|
| Cost | Cost build-up by group, the ex-works note, the editable bill of materials and the editable man-hours by activity |
| Components | The cards in fabrication order and the live sketch (Chapter 2) |
| Cut list | Every pipe piece: size, schedule, cut length, end preparation, piece mark |
| Welds and checks | The weld register with type, size, wall and NDT by weld (tick to choose), then the fabrication checks and open items |
| Schedule | Bar chart: drawing approval, procurement, fabrication with NDT and test, finishing and dispatch |
| Drawings | The four A4 sheets (section 4.3) |
| Report | The estimate report as it will print |

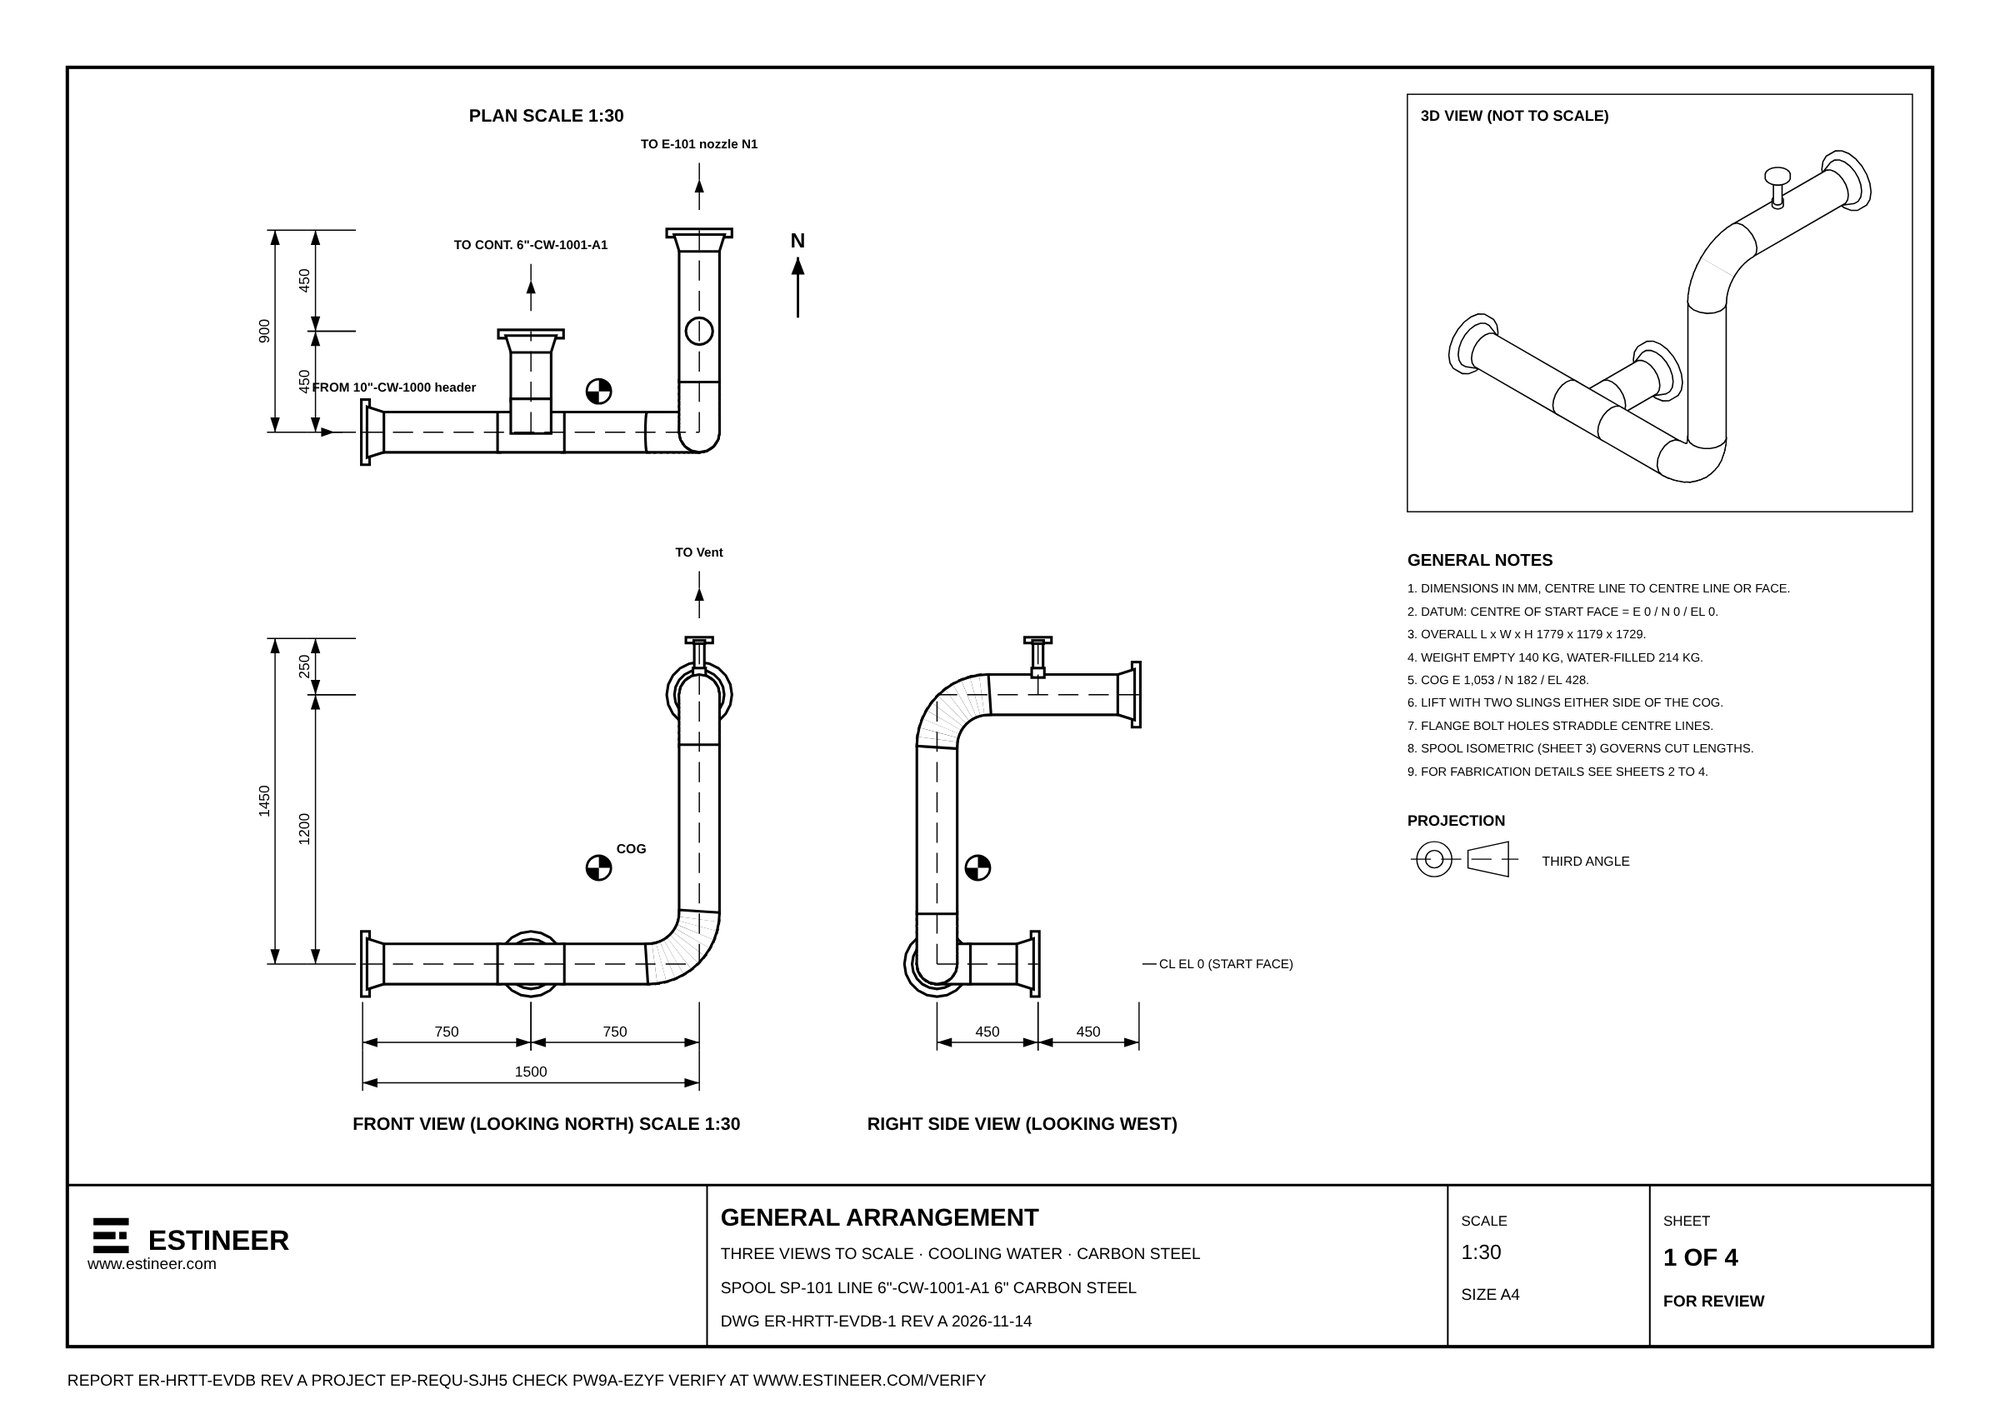
Four A4 landscape sheets, black on white, generated from the same model as the price. Each carries the Estineer title block, the spool tag and line, a drawing number, the revision and the words FOR REVIEW.


The full report opens with a cover page: the 3D picture, the spool, size and class, and a table with project, client, equipment, prepared by, document number and date. The disclaimer is printed once, on the cover. The body follows, with bookmarks, a contents list that links to each section and searchable text:
| No. | Section | Content |
|---|---|---|
| 1 | Estimate summary | Direct cost, price, man-hours, duration, weight; cost build-up |
| 2 | Spool data | Tag, line, service, material, specifications, ends, branches, envelope, weights, test, finish, NDT |
| 3 | Design basis and fabrication checks | Statement that the design is by others; checks and open items |
| 4 | Bill of materials and MTO | Items, quantities, weights, prices |
| 5 | Cut list | Pipe pieces and lengths |
| 6 | Weld register | Every weld and its inspection |
| 7 | Labour man-hours | Every activity with quantity, unit rate, factor and hours |
| 8 | Basis of estimate: assumptions | Every allowance the tool used |
| 9 | Exclusions | What the price does not include |
The four drawing sheets follow the report in the same PDF. “Drawings only (PDF)” saves the four sheets alone.
| File | Content |
|---|---|
| Excel | Sheets Cover, Summary, Materials, Man-hours, Spool data, Cut list, Welds, Checks, Assumptions, Exclusions and MTO. Rates, contingency and markup are named input cells; the cost and price are live formulas, so you can change a rate and see the price move. |
| Word | The report as an editable document with the cover, the tables and the drawings as pictures. |
| MTO (Excel, CSV) | The material take-off for purchasing: one line per item with quantity, unit, weight and price. |
Each purchased report carries a report id (ER-XXXX-XXXX) with its revision, a project id (EP-XXXX-XXXX) and a check code. The check code is a fingerprint of the inputs, the engine version and the database. Anyone can confirm a report at estineer.com/verify: the page says whether the report is genuine and when it was issued, without showing the price or the buyer. The ids are printed on the cover, in every page footer, under every drawing frame and in the Excel and Word files.
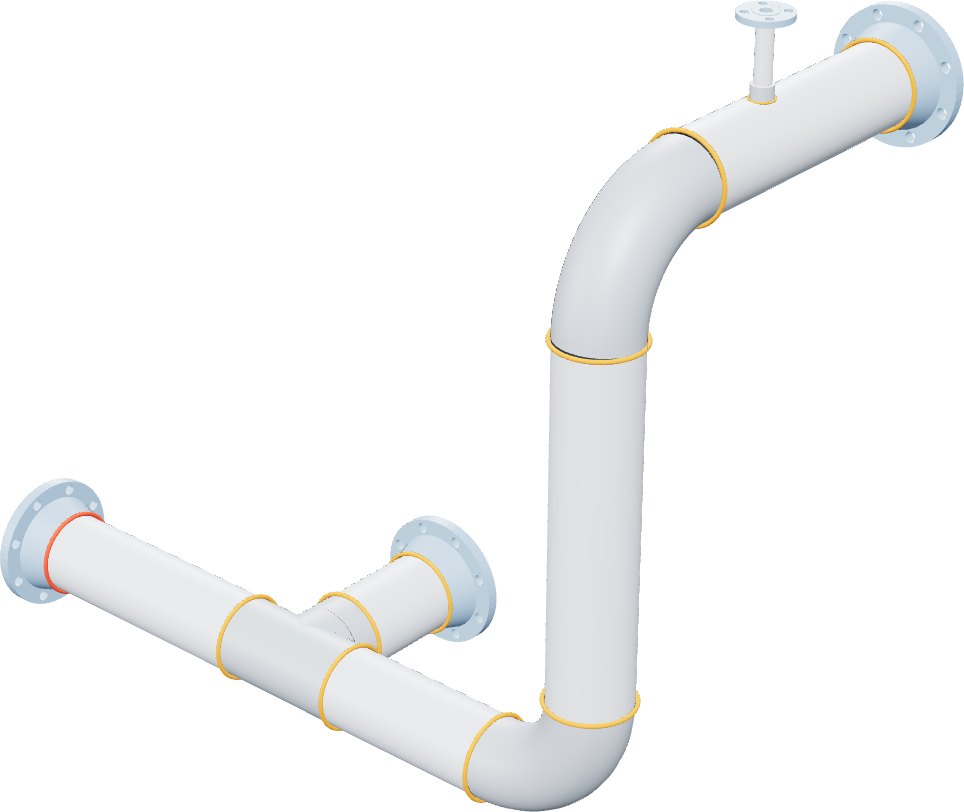
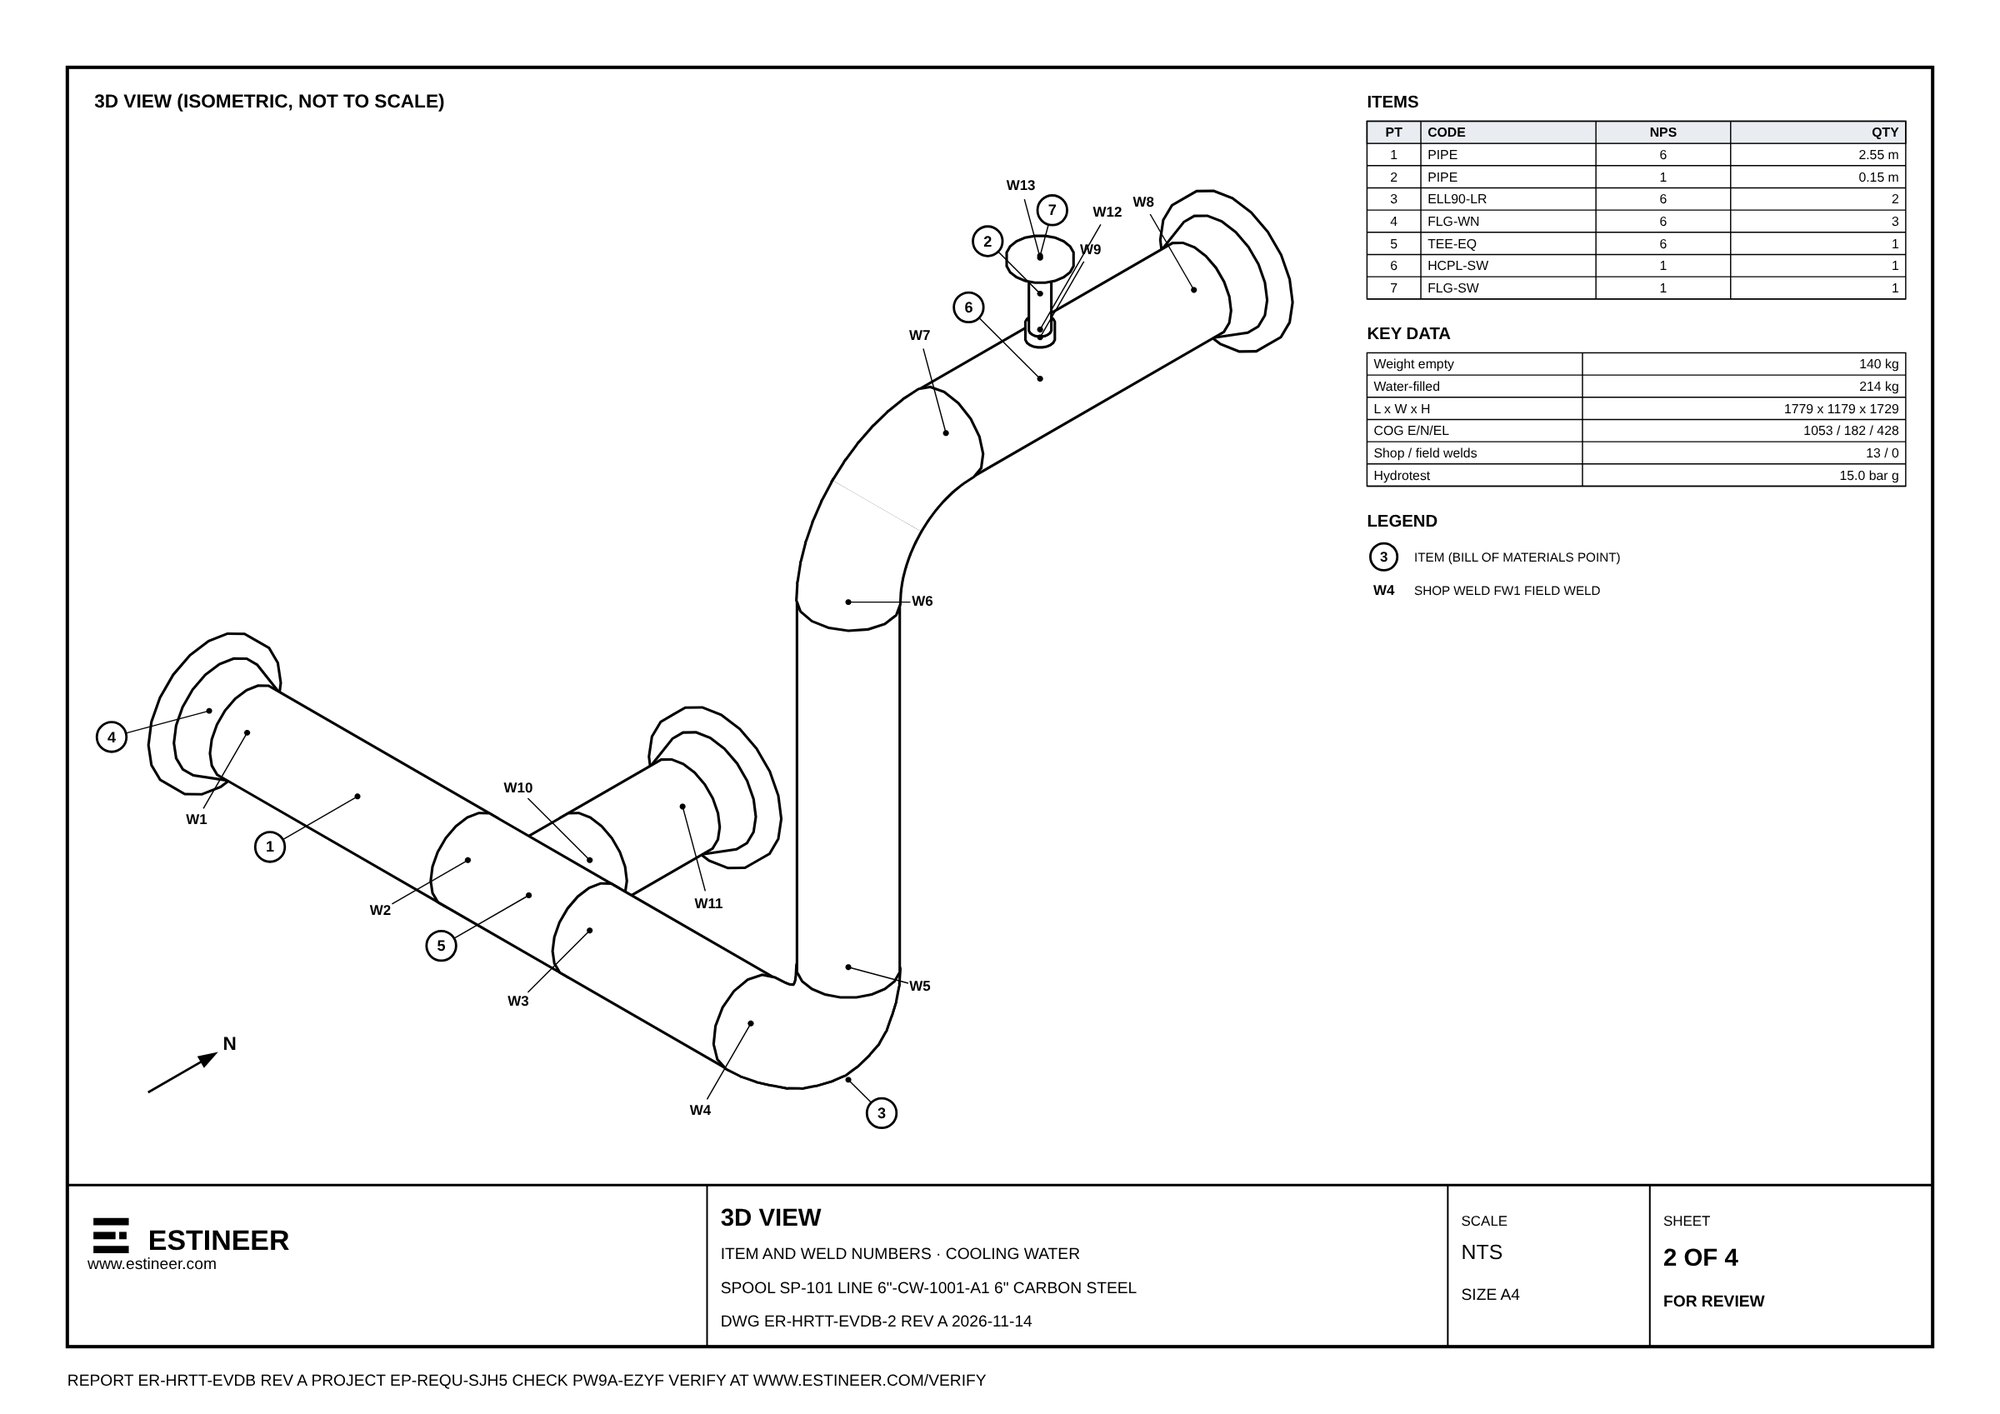
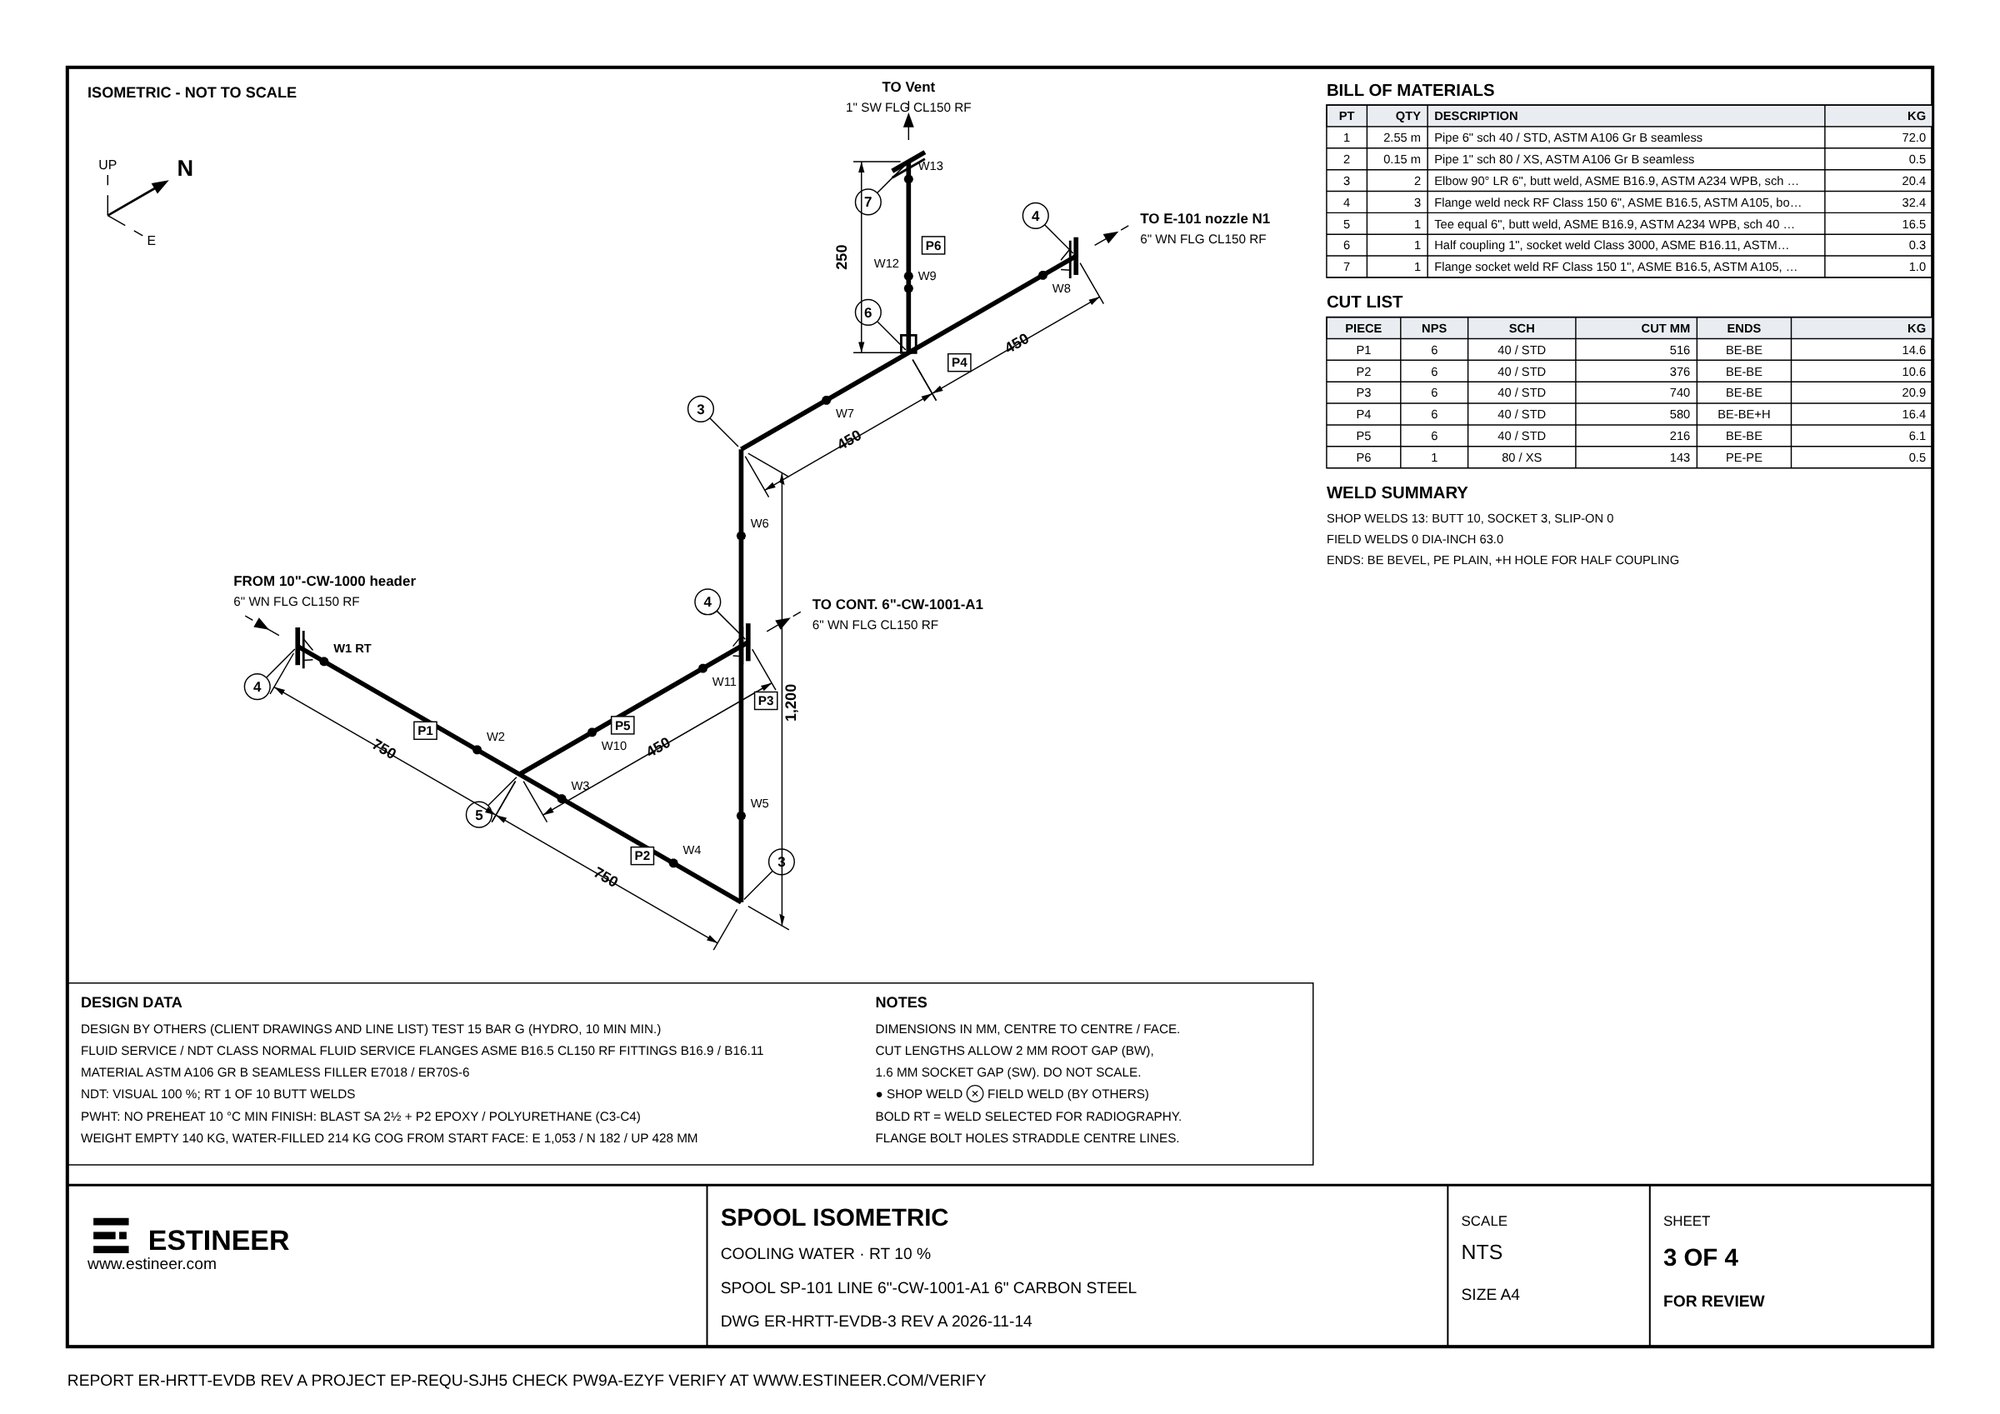
SP-101 is the example the tool opens with: a 6" carbon steel cooling-water spool with a branch tee, two elbows and a 1" vent. Every number in this chapter is produced by the engine when the manual is built, so it matches the tool exactly.
| Spool tag / line | SP-101 / 6"-CW-1001-A1 |
| Service | Cooling water |
| Material | Carbon steel, ASTM A106 Gr B seamless |
| Main size, schedule, class | NPS 6, 40 / STD, Class 150 |
| Fluid service | Normal fluid service |
| Start end | Weld neck flange, from 10"-CW-1000 header |
| Components | pipe 750 mm; tee equal NPS 6 left, branch 450 mm, WN; pipe 750 mm; elbow 90° LR up; pipe 1,200 mm; elbow 90° LR left; pipe 450 mm; half coupling NPS 1 up, branch 250 mm, SW; pipe 450 mm |
| Finish end | Weld neck flange, to E-101 nozzle N1 |
| Finish and test | P2 Epoxy / polyurethane; hydrotest 15 bar g; NDT default |
| Rates | shop 110, engineering 150, NDT 160 AUD/h; contingency 10 %; markup 15 %; crew 2, 38 h/week |

The route gives an envelope of 1.78 x 1.73 x 1.18 m, inside the 12.0 x 2.4 x 2.6 m truck envelope. The pipe is cut into 6 pieces:
| Piece | NPS | Schedule | Cut, mm | Ends |
|---|---|---|---|---|
| P1 | 6" | 40 / STD | 516 | BE-BE |
| P2 | 6" | 40 / STD | 376 | BE-BE |
| P3 | 6" | 40 / STD | 740 | BE-BE |
| P4 | 6" | 40 / STD | 580 | BE-BE |
| P5 | 6" | 40 / STD | 216 | BE-BE |
| P6 | 1" | 80 / XS | 143 | PE-PE |
Piece P1 is worked in section 3.2: 750 − 89 − 143 − 2 = 516 mm. There are 13 shop welds: 10 butt, 1 half coupling, 2 socket. With normal fluid service, radiography is 5 % of the butt welds, which rounds up to 1 weld.
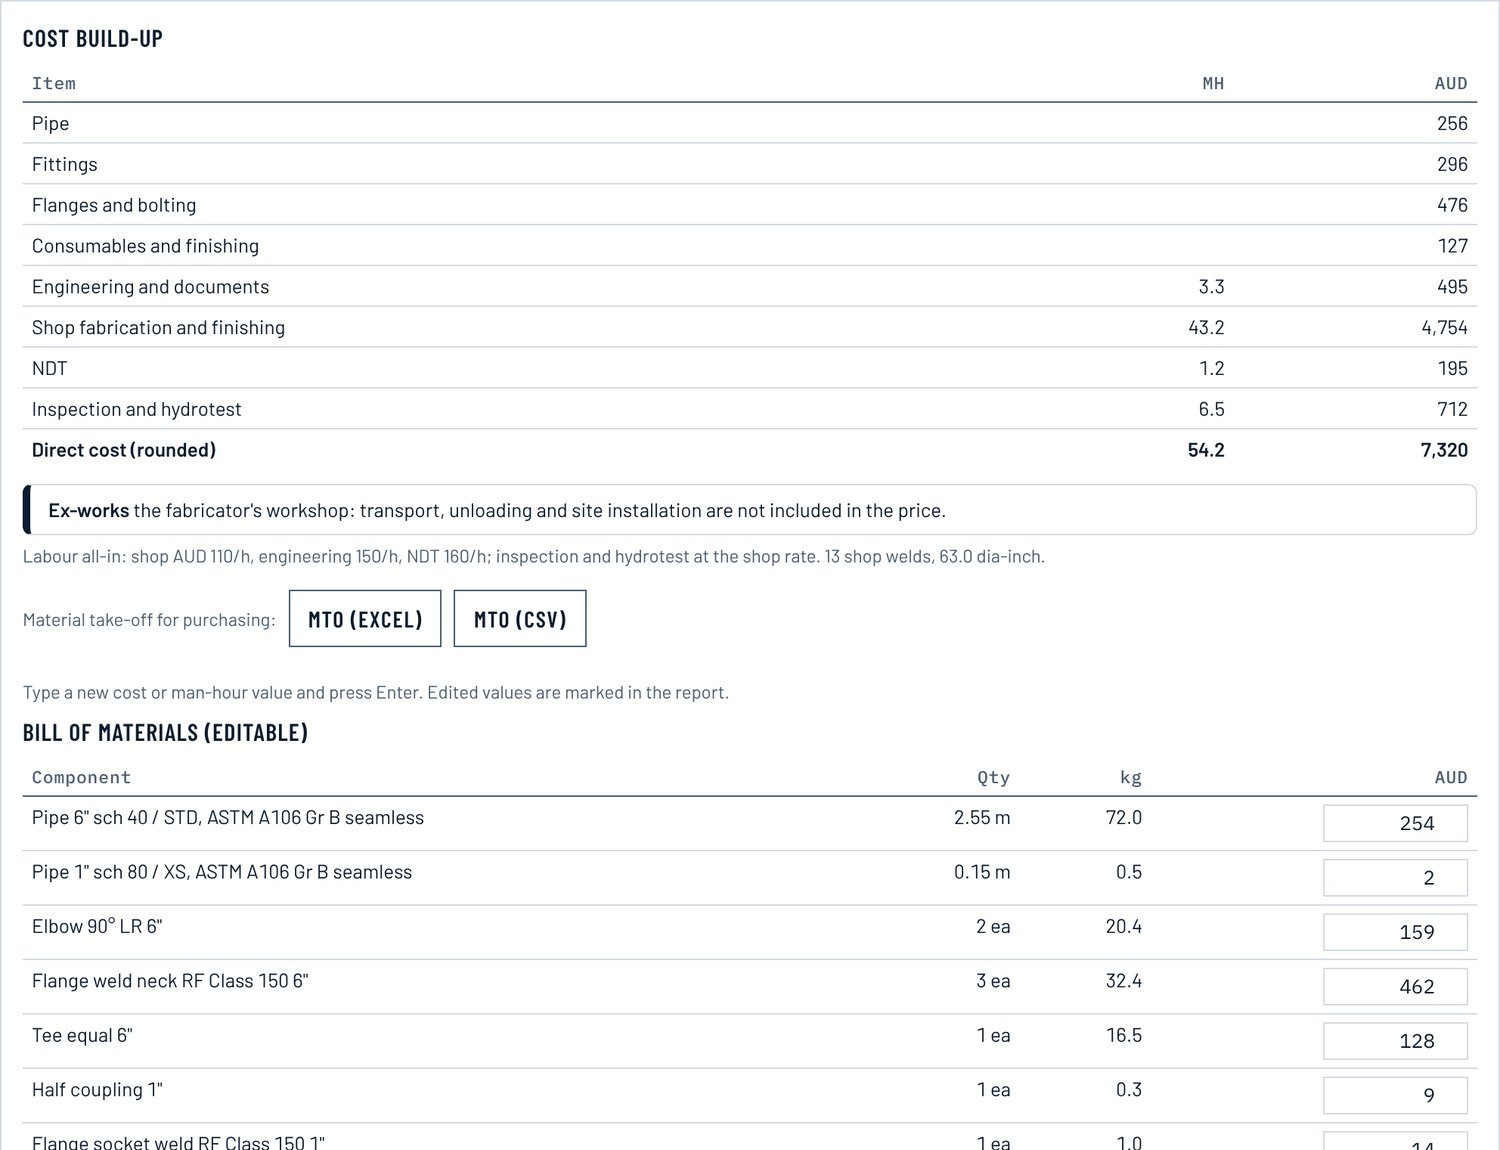
Catalogue prices in USD × 1.4706 = AUD. Pipe includes the 5 % cutting loss.
| Item | Quantity | kg | AUD |
|---|---|---|---|
| Pipe 6" sch 40 / STD, ASTM A106 Gr B seamless | 2.55 m | 72.0 | 254.27 |
| Pipe 1" sch 80 / XS, ASTM A106 Gr B seamless | 0.15 m | 0.5 | 1.72 |
| Elbow 90° LR 6" | 2.00 ea | 20.4 | 159.00 |
| Flange weld neck RF Class 150 6" | 3.00 ea | 32.4 | 462.18 |
| Tee equal 6" | 1.00 ea | 16.5 | 128.44 |
| Half coupling 1" | 1.00 ea | 0.3 | 8.81 |
| Flange socket weld RF Class 150 1" | 1.00 ea | 1.0 | 14.26 |
| Welding consumables (E7018 / ER70S-6) | 4.39 kg | 4.4 | 58.13 |
| Abrasive for blasting Sa 2½ | 48.70 kg | 0.0 | 28.66 |
| Paint system P2 Epoxy / polyurethane | 2.21 m2 | 0.0 | 40.16 |
| Materials total | 147.5 | 1,155.63 |
Empty 139.6 kg; water 74.1 kg; full of water for the test 213.7 kg. Centre of gravity from the start face: E 1,053 / N 182 / Up 428 mm, shown on the GA drawing.
| ID | Activity | Quantity | MH/unit | Factor | MH |
|---|---|---|---|---|---|
| HAND-6 | Pipe handling in shop NPS 6 sch 40 / STD | 2.43 m | 0.200 | 1 | 0.49 |
| CUT-6 | Pipe cutting, machine NPS 6 (one cut per piece) | 5 ea | 0.681 | 1 | 3.41 |
| BEV-6 | Pipe bevelling, machine NPS 6 | 10 ea | 0.445 | 1 | 4.45 |
| HAND-1 | Pipe handling in shop NPS 1 sch 80 / XS | 0.14 m | 0.103 | 1 | 0.01 |
| CUT-1 | Pipe cutting, machine NPS 1 (one cut per piece) | 1 ea | 0.259 | 1 | 0.26 |
| BW-6-7.11 | Butt weld, manual NPS 6 wall 7.11 mm | 7 joint | 2.780 | 1 | 19.46 |
| HC-1 | Half coupling NPS 1 welded to run pipe (incl. hole) | 1 ea | 1.580 | 1 | 1.58 |
| SW-1 | Socket weld NPS 1 Class 3000 | 2 joint | 0.614 | 1 | 1.23 |
| WN-6 | Weld neck flange attachment NPS 6 Class 150 (incl. butt weld, | 3 ea | 3.860 | 1 | 11.58 |
| QC | Fit-up checks, marking and dimensional inspection | 1 spool | 1.150 | 1 | 1.15 |
| BLAST | Abrasive blasting Sa 2½ | 2.21 m2 | 0.100 | 1 | 0.22 |
| PAINT | Painting P2 Epoxy / polyurethane, 3 coats | 2.21 m2 | 0.240 | 1 | 0.53 |
| RT | Radiography (RT): 1 of 10 butt welds | 1 ea | 1.220 | 1 | 1.22 |
| HT-start | Hydrotest, flanged end (start, NPS 6) | 1 end | 1.440 | 1 | 1.44 |
| HT-end | Hydrotest, flanged end (end, NPS 6) | 1 end | 1.440 | 1 | 1.44 |
| HT-branch 1 | Hydrotest, flanged end (branch 1, NPS 6) | 1 end | 1.440 | 1 | 1.44 |
| HT-branch 2 | Hydrotest, flanged end (branch 2, NPS 1) | 1 end | 1.000 | 1 | 1.00 |
| ENG | Spool drawing check, weld map, test pack and data book | 1 spool | 3.300 | 1 | 3.30 |
| Total | 54.2 |
By stage: engineering 3.30, shop 43.21, NDT 1.22, test 6.47 MH. Engineering = 2 + 0.1 × 13 welds = 3.3 MH.
The tool shows direct cost AUD 7,320 and indicative price AUD 9,260, excluding GST, ex works.
Shop, test and NDT hours 50.9 MH / (crew 2 x 38 h) = 0.67 weeks of fabrication.
| Stage | Starts, week | Lasts, weeks |
|---|---|---|
| Drawing approval | 0.0 | 0.5 |
| Material procurement | 0.5 | 2.0 |
| Fabrication, NDT and test | 2.5 | 1.0 |
| Finishing and dispatch | 3.5 | 0.5 |
Duration: 4 weeks from order to dispatch.
| Item | Limit |
|---|---|
| Sizes | NPS ½ to 24; schedules as in the catalogue for each material and size |
| Route | 1 to 12 straight runs, each 20 mm to 12,000 mm; up to 6 branches |
| Flanges | Class 150 to 1500; socket-weld flanges NPS 3 and smaller |
| Test pressure | Above 0 and at most 400 bar g; checked against the flange class |
| Preheat | 5 to 300 °C |
| Commercial inputs | Rates and exchange rate above 0; contingency and markup 0 to 100 %; crew 1 to 50; 1 to 84 hours per week; edited costs and hours zero or more |
| Transport | Spools larger than 12.0 x 2.4 x 2.6 m are warned: split with a field weld or plan an oversize load |
| Message | What to do |
|---|---|
| Add a pipe before this item | Two fittings cannot touch: put a pipe card of at least 20 mm between them. |
| Straight run is too short for its fittings | The centre-line length is shorter than the fittings on it; check the isometric dimension. |
| The reducer outlet is the same as the pipe before it | Choose a smaller outlet size, or delete the reducer. |
| Forward / back are for a vertical pipe | On a horizontal pipe turn up, down, left or right. |
| MT does not work on stainless steel | Use PT for surface examination of stainless welds. |
| Hydrotest pressure not given | Enter the test pressure from the client's line list; 15 bar g is used meanwhile. |
| Larger than a standard truck load | Add a field weld (two spools) or allow for an oversize transport. |
| … must be more than zero / at most … | A rate, percentage or crew value is outside the allowed range (Chapter 2). |
No. The design is by others: the wall thickness and class come from the client's pipe class. The tool checks fabrication points only, and says so in the report.
Isometric dimensions are centre to centre or face to centre. The cut length deducts the fittings and the weld gaps (section 3.2).
Yes. Type a new value in the bill of materials or the man-hours table in the Cost tab. The report marks the line as set by you and keeps the tool value for reference.
Stainless handling and cutting carry a factor of 1.2, welding 1.46, plus 0.6 h per joint for purging and cleaning, and pickling replaces painting.
No. The price is ex works: the fabricator's workshop. Transport, unloading and site installation are excluded.
Yes: the same inputs, engine version and database always give the same numbers and the same check code.
It is usually more than one spool on the isometric. Enter each spool separately, or use Pipeline Spool Fabrication, which splits a whole line into spools.
| BE / PE | Bevelled end for a butt weld / plain end for a socket weld |
| BW / SW | Butt weld / socket weld |
| CoG | Centre of gravity |
| LR / SR | Long-radius (1.5 D) / short-radius (1.0 D) elbow |
| MH | Man-hour |
| MTO | Material take-off |
| NDT: RT, UT, MT, PT | Radiography, ultrasonic, magnetic particle, dye penetrant |
| NPS | Nominal pipe size, inch |
| PWHT | Post-weld heat treatment |
| Spool | A shop-fabricated piece of piping between field joints |
| WN / SO / BL | Weld neck / slip-on / blind flange |
| WPS | Welding procedure specification |